Engineered Warehouse Pallet Racking Portfolio
Explore China's most reliable, precision-engineered warehouse storage systems. Designed in compliance with FEM 10.2.02 and RMI/ANSI MH16.1 standards for optimal load-bearing safety, seismic durability, and high-density throughput.
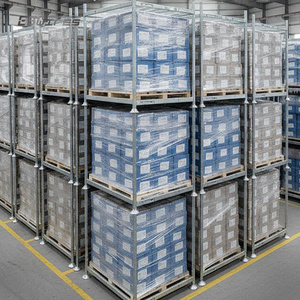
Sturdy Structure Mild Steel Q235 Heavy Duty Steel Detachable Type Stacking Post Pallet Rack
Engineered from premium Q235B mild structural steel, offering modular stackability up to 4-high. Eliminates permanent aisle space while protecting bulk payload units.
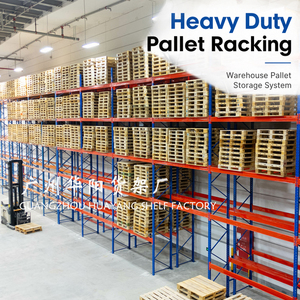
3000KG Per Level Heavy Duty Pallet Rack Industrial Warehouse Storage Steel Shelving Adjustable Pallet Racking System
Heavy-duty selective beam racking supporting up to 3,000 kg per level. Equipped with 75mm beam pitch adjustability, dual safety pin locks, and durable powder coating.
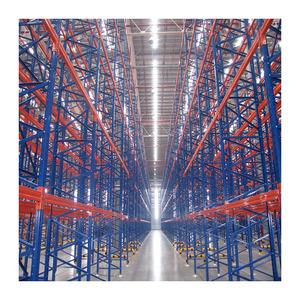
Mracking Heavy Duty Industrial Palletized Racking with a Capacity of 1000-4000kg Industrial Storage Racking
High-capacity palletized racking optimized for distribution centers. Customizable beam lengths up to 3900mm with load capacities tested up to 4,000kg per tier.
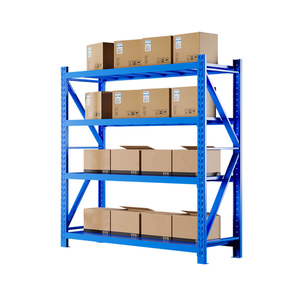
Industrial Warehouse Storage 5-Layer Pallet Racking System with Tire Rack Slotted Angle Rack Stacking Racks & Shelves
Versatile 5-layer multi-tier warehouse system combining selective pallet positions with custom slotted angle tire racking for specialized automotive logistics.
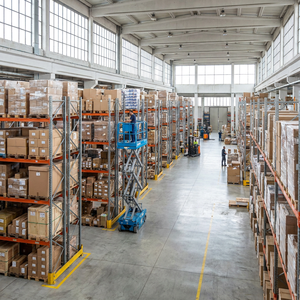
Professional Heavy Duty Pallet Rack Supplier Warehouse Storage System Manufacturer
Tailor-made industrial racking engineered for maximum height clearance and floor load utilization. Built with cold-rolled steel profiles for structural longevity.
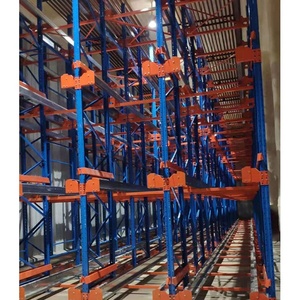
Customized Steel Pallet Rack Stacking Racks & Shelves Warehouse Storage Rack Heavy Duty Shuttle Racking for Industrial
Semi-automated radio pallet shuttle system designed for ultra-dense FIFO/LIFO cold storage and high-turnover logistics. Maximize volume utilization by up to 85%.
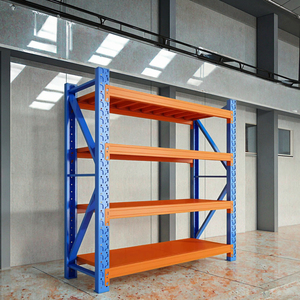
Adjustable Heavy Duty Steel Industrial Rack with Corrosion Protection 5-Layer Boltless Design Competitive Price Shelves
Boltless interlocking steel structure featuring anti-corrosion electrostatic epoxy finishing. Quick snap-in installation reduces onsite assembly time by 40%.
Heavy Duty Warehouse Pallet Racks Customized High Load 1000kg-5000kg Industrial Storage Selective Steel Pallet Racking System
Ultra-high capacity selective industrial racking supporting up to 5,000kg per beam level. Designed for heavy manufacturing, machinery components, and automotive raw materials.
Why Global Enterprise Logistics Trust Our Manufacturing Superiority
As China’s leading warehouse pallet racking system supplier and exporter, we combine advanced steel metallurgy, robotic automation, and stringent structural safety compliance to deliver unmatched ROI for overseas procurement teams.
Q235B & Q355B High-Yield Steel Metallurgy
We source prime cold-rolled steel coils exclusively from Tier-1 state mills (BaoSteel & Shougang Group). Guaranteed yield strength of 235–355 MPa ensures zero structural deflection under maximum rated loading limits.
Robotic Welding & Automated Powder Coating
Utilizing Panasonic 6-axis robotic welding cells for 100% seam penetration. Finished on Swiss Gema automatic electrostatic powder coating lines, offering 60-80μm coating thickness for superior rust resistance.
Seismic & Structural FEM 10.2.02 Compliance
All structural designs undergo rigorous Finite Element Method (FEM) computer simulation and physical destructive testing to comply with international RMI (USA), AS4084-2012 (Australia), and CE standards.
Industrial Engineering Specifications & Structural Analysis
Information Gain Analysis: Understanding the mechanical properties and structural differences across industrial warehouse pallet racking systems is critical to optimizing safety and Total Cost of Ownership (TCO).
Structural Steel Roll-Forming Mechanics & Safety Margin
Our heavy-duty upright frames are engineered using multi-stage cold roll-forming machines with up to 24 rolling stations. This continuous cold-working process increases steel yield strength by over 15% relative to basic flat plates. Furthermore, column profiles feature omega-shaped geometry with multiple stiffening ribs to resist torsional buckling caused by incidental forklift impact.
In selective pallet racking systems, beam connectors utilize 3 or 4-hook claw attachments stamped from heavy gauge steel plate. Each connector is fitted with an automatic mechanical spring lock that prevents accidental dislodgement from upward forklift mast movement—a non-negotiable safety feature required under ANSI MH16.1.
| Racking System Type | Material Grade | Max Load / Level | Volume Utilization | Handling Equipment Required | Key Standard Compliance |
|---|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B Steel | 1,000 - 4,500 kg | 40% - 50% | Standard Counterbalance / Reach Truck | FEM 10.2.02, RMI, ISO 9001 |
| Pallet Shuttle System | Q355B Cold Rolled | 1,500 kg / Pallet | 80% - 88% | Radio Shuttle Cart + Forklift | CE, ISO 14001, EN 15512 |
| Drive-In / Drive-Thru | Q235B Heavy Duty | 1,000 - 1,800 kg | 65% - 75% | Reach Truck / Specialized Narrow Truck | ANSI MH16.1, AS 4084 |
| Push-Back Racking | Q235B Structural Cart | 1,200 kg / Cart | 60% - 70% | Standard Forklift | FEM 10.2.02, RMI |
| Heavy Duty Cantilever | H-Section Hot Rolled Steel | 1,000 - 6,000 kg / Arm | Custom Layout | Side Loader / Heavy Counterbalance | GB/T 13793-2008, CE |
Future Procurement Trends in Industrial Warehouse Racking (2025–2030)
Global supply chain evolution is forcing warehouse managers and procurement directors to adapt to rapid automation, stringent carbon mandates, and intelligent warehouse infrastructure.
1. Convergence of Structural Racking with AGVs & AMRs
Traditional pallet racking is undergoing structural redesign to accommodate Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Procurement demands now specify tight floor levelness tolerances (Superflat Floors FF/FL metrics) and specialized rack-bottom guide rails with magnetic floor strips to enable seamless robotic positioning.
2. High-Density Radio Shuttle & AS/RS Dominance
With industrial land acquisition costs rising globally by 12-18% annually, enterprise buyers are shifting capital expenditures from horizontal expansion toward vertical high-density systems. Semi-automated Pallet Shuttle systems and Automated Storage and Retrieval Systems (AS/RS) capable of reaching heights of 30+ meters are becoming the global standard for cold storage and FMCG hubs.
3. Green Steel & Low-VOC Powder Coating Mandates
ESG compliance now directly impacts international supply chain bidding. Top global exporters in China are adopting recycled green steel billets and switching from solvent-based paints to 100% recyclable, zero-VOC electrostatic epoxy powder coatings that drastically lower carbon emissions across the production lifecycle.
4. Smart Sensor Integration & Collision Monitoring
Next-generation industrial pallet racking incorporates IoT impact sensors mounted on upright guards and critical beam connections. Real-time telemetry alerts facility directors to structural deformities or forklift collisions instantly, ensuring proactive maintenance before catastrophic rack failure occurs.
Strategic Sourcing SOP: How to Import Racking Systems from China Risk-Free
A step-by-step procurement playbook for logistics managers, global buyers, and warehouse engineers to guarantee product quality and compliance.
Before issuing a Purchase Order (PO), verify your warehouse slab concrete compressive strength (minimum C25/C30 grade recommended) and floor thickness (at least 150-200mm for heavy duty anchors). Work with our engineering team to generate 3D AutoCad layouts detailing forklift aisle turning radii (AST - Right Angle Stacking Aisle), sprinkler clearance, and light fixture spacing.
Require Mill Test Certificates (MTC) according to EN 10204 3.1 verifying chemical composition (Carbon, Manganese, Silicon content) and mechanical tensile testing for each steel batch. Demand third-party ultrasonic weld inspection reports and neutral salt spray testing (ISO 9227) showing 500+ hours without red rust formation for outdoor or humid applications.
Shipping freight costs directly influence landed cost per pallet position. Our structural components feature modular knock-down designs packed with specialized steel banding, timber dunnage, and moisture-proof plastic wrap. High-cube 40HQ containers are nested to achieve up to 26 metric tons maximum payload weight utilization without damaging powder-coated surfaces.
Frequently Asked Questions (Sourcing & Technical FAQ)
Direct answers to essential technical and procurement questions asked by international project buyers.
Q235B steel (Yield Strength 235 MPa) is the standard cost-effective steel grade suitable for standard selective racking with beam loads up to 2,500kg. For ultra-heavy loads (3,000kg to 5,000kg/level), high-bay installations exceeding 10 meters, or high seismic zone projects, Q355B steel (Yield Strength 355 MPa) is specified to reduce structural dead weight while providing superior tensile strength and resistance against seismic sway.
We supply full engineering compliance packages with every export shipment, including: Factory Structural Calculation Sheets, Mill Test Certificates (EN 10204 3.1), ISO 9001 / ISO 14001 certificates, CE Certificate of Conformity for Shuttle/ASRS components, and detailed CAD installation drawings stamped by certified structural engineers.
Standard manufacturing lead time for standard selective racking (1-5 container loads) is 15 to 20 days upon deposit confirmation. For custom large-scale distribution centers (10+ 40HQ containers or automated shuttle systems), production schedules range from 25 to 35 days. Our facility operates 6 automated roll-forming lines delivering up to 8,000 tons per month.
Yes. Every warehouse layout has unique structural column spacing and clear height constraints. We offer completely tailored dimensions: Upright depth (600mm to 1500mm), Upright height (up to 15 meters in single section), Beam lengths (1000mm to 3900mm), and pitch adjustability (50mm, 75mm, or 76.2mm pitch). Custom RAL powder coating colors are available to align with corporate brand guidelines.
We provide three installation assistance tiers: 1) Comprehensive 3D assembly manuals and video walk-throughs for local installation teams; 2) Remote real-time video guidance from our project engineering team; 3) Dispatching senior installation supervisors on-site anywhere in the world to oversee assembly, anchoring, and final vertical alignment tolerance checks.
Optimize Your Warehouse Density & Request a Technical Proposal Today
Submit your warehouse floor plans or pallet storage requirements. Our structural engineers will deliver a free 3D CAD layout, load capacity calculation, and competitive factory-direct quote within 24 hours.
Get a Quote